How to Choose the Best Aluminum Die Cast Mold?

Choosing the right Aluminum Die Cast Mold is rarely a simple price comparison. The mold must match the alloy, part geometry, machine capacity, and production volume. A small mismatch can create flashing, porosity, short shots, or premature tool failure. These problems often appear after hundreds of cycles, when correction becomes expensive.

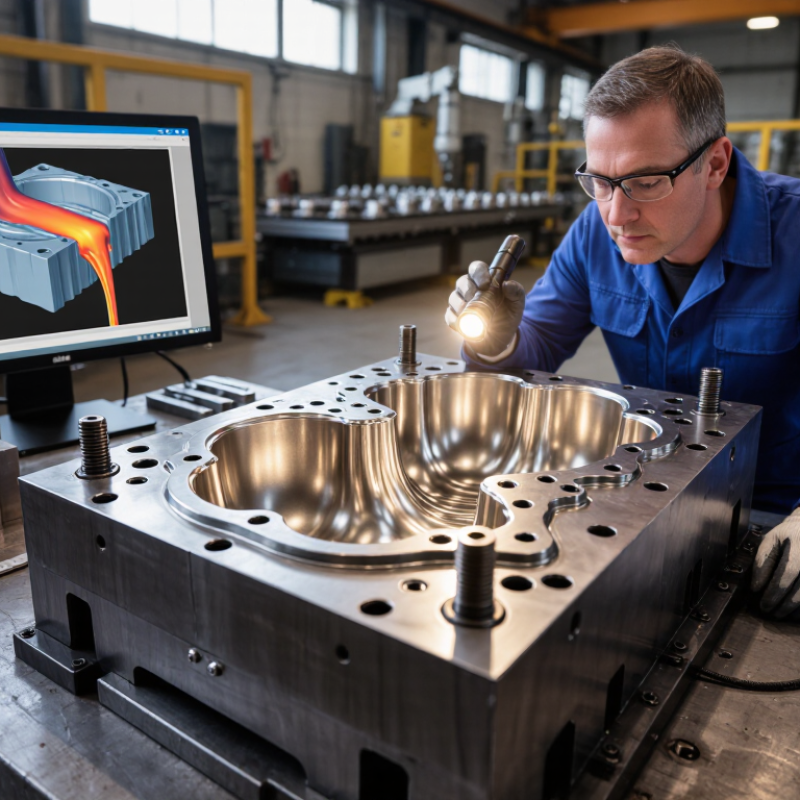
John Campbell, a leading casting researcher and author of Complete Casting Handbook, stated, “The quality of a casting is determined by the quality of the liquid metal.” His observation also applies to mold design. Clean metal cannot compensate for poor venting, uneven cooling, or an unsuitable gate system. A reliable Aluminum Die Cast Mold should control metal flow and remove heat consistently. Engineers should examine mold steel, cavity finish, cooling channels, ejector placement, and expected thermal fatigue. A polished cavity may look impressive, but it will not solve a weak cooling layout.

Real production experience matters. Ask whether the supplier has tested similar aluminum alloys and part shapes. Request evidence, such as filling simulations, dimensional reports, trial-run records, and maintenance plans. Check how the mold performs after repeated thermal cycles, not only during its first sample run. That detail is often missed. Sometimes, the cheapest mold becomes the most expensive choice.

This guide explains how to compare mold materials, design features, supplier capability, service life, and total cost. It also considers practical risks that drawings may hide. No selection method is perfect. However, careful questions can prevent avoidable failures before steel is cut.
How to Choose the Best Aluminum Die Cast Mold?

Aluminum Die Cast Mold Basics: Alloys, H13 Steel, and 30–150 MPa Pressure

How to Choose the Best Aluminum Die Cast Mold?

Aluminum die cast mold selection starts with the alloy, not the mold drawing. Silicon-rich alloys improve fluidity but can increase mold erosion. Copper-containing alloys may demand stronger thermal control. Check the alloy’s filling temperature, shrinkage, and cooling behavior before choosing steel. Small differences can change flash, porosity, and cycle time.

H13 hot-work tool steel remains a practical choice for demanding dies. Its toughness helps resist thermal cracking during repeated heating and cooling. Proper heat treatment matters as much as the steel grade. A poorly treated insert can fail early, even with careful machining.

In production trials, I would inspect gate areas, corners, and ejector holes first. Those locations often show damage before flat surfaces do.

Pressure also changes the mold’s working conditions. Many high-pressure aluminum casting systems operate between 30 and 150 MPa. Lower pressure may reduce flash but can leave thin ribs unfilled. Higher pressure can improve detail, while increasing wear, clamping demand, and porosity risk. The correct value depends on wall thickness, gate design, alloy temperature, and machine response.

Do not select pressure from a chart alone. Test it.

Cooling channels should follow hot spots rather than a perfect geometric pattern. That sounds simple. It is not. Uneven cooling can bend the die or create unstable dimensions. Mold makers should record thermal cycles, inspect crack growth, and adjust maintenance intervals from real data. A universal mold formula does not exist; even experienced teams sometimes discover that their first design needs revision.

Define Part Requirements: Wall Thickness, Tolerances, and 0.1-Second Filling

Choosing the best aluminum die cast mold starts with the part, not the machine. Define wall thickness, tolerances, and filling behavior before cutting steel. NADCA’s 2021 Product Specification Standards indicate that aluminum walls often fall near 1.5–2.5 mm, depending on flow length, alloy, and surface requirements. A thinner wall is not automatically better. Long, thin sections can create cold shuts, trapped air, and early die wear.

Measure critical dimensions clearly. NADCA tolerance tables distinguish commercial and precision grades; values near ±0.05 mm over 25 mm require stable tooling, temperature, and process control. ASM Handbook, Volume 15, also stresses that dimensional variation increases with part size, ejection movement, and uneven cooling. Give the mold designer datum points, shrinkage assumptions, and inspection locations. Guesswork is expensive.

A 0.1-second filling target is common for thin-wall high-pressure die casting, but it is not universal. Filling too slowly may freeze the metal before the cavity closes. Filling too quickly can increase air entrapment and flash. I have seen projects chase 0.1 seconds while ignoring gate position. That was a mistake. Simulation should compare fill time, velocity, pressure, and venting together. The chosen mold must make the metal reach the last rib cleanly, without forcing every feature into an extreme process window.

Compare Mold Designs: Two-Plate, Three-Plate, Slides, and Ejector Systems

Choosing an aluminum die cast mold starts with part geometry, not a familiar mold layout. In production reviews, I examine the parting line, wall thickness, draft, and expected shot volume. A two-plate design is often the practical baseline. It has a simpler feed path, fewer moving components, and easier maintenance. That simplicity can reduce setup time. Yet it may leave a visible gate mark or limit gate placement. For parts needing multiple gates or controlled filling, a three-plate design offers more layout freedom. Its extra plate adds movement, alignment points, and cleaning work. I would not select it automatically.

Slides deserve careful attention when ribs, windows, or undercuts block direct ejection. A slide can preserve useful geometry, but it needs durable guidance, lubrication access, and enough travel clearance. Check where aluminum flash might collect. Small gaps become expensive defects. The ejector system also shapes reliability. Ejector pins should push near balanced areas, while sleeves or blades may suit holes and thin walls. Uneven force can bend a hot casting or leave stress marks. In one review, I underestimated ejection resistance because the draft looked adequate on a drawing. The first trial proved otherwise. That was a useful correction. Simulation helps, but it cannot replace measurements from actual castings. Record cycle time, flash, sticking, and pin marks after each trial. Perfect designs do not exist. Good designs expose their compromises early.

Evaluate Thermal Performance: 150–250°C Preheating and Cooling Channels

How to Choose the Best Aluminum Die Cast Mold?

Thermal performance should guide mold selection, not just cavity geometry. Preheating the die to 150–250°C reduces thermal shock during aluminum injection. NADCA’s 2021 Product Specification Standards identifies controlled die temperature as a key factor in reducing heat checking and premature failure. In practice, I use surface thermocouples near gates, ribs, and sharp corners. Measure, do not guess. A 20°C difference across one cavity can create uneven filling, soldering, or dimensional drift.

Cooling channels need equal attention. The channel layout should remove heat without creating cold spots near thin walls. According to the International Energy Agency’s energy-efficiency research on metal casting, process stability depends heavily on controlling repeated heating and cooling cycles. Straight channels may be easy to machine, but they often leave hot areas around deep cores. Conformal or closely spaced passages can improve uniformity, although they may increase manufacturing cost and inspection demands. Flow rate, coolant temperature, channel diameter, and distance from the cavity surface should be recorded during trials.

Thermal simulation is useful, but it is not reality. I have seen models predict balanced cooling while measured corner temperatures remained high. That gap deserves investigation. The Die Casting Research Foundation reports that thermal fatigue is strongly linked to cyclic temperature variation and local stress concentration. Choose mold steel, venting, and cooling design together. Also allow enough preheating time; a cold outer block can distort readings. The best mold is not always the fastest one. It is the one that holds stable temperatures through thousands of cycles.

Select Mold Life and Cost: 100,000–200,000 Shots, Maintenance, and ROI

Choosing an aluminum die cast mold starts with expected shot life, not the lowest quotation. A practical planning range is 100,000 to 200,000 shots. NADCA’s Product Specification Standards emphasize thermal fatigue, soldering, erosion, and cooling design as major life factors. Aluminum alloys with high silicon content can accelerate wear around gates and slides. That detail is easy to miss.

Assume a mold costs $30,000. At 100,000 shots, its tooling cost is $0.30 per shot. At 200,000 shots, the cost falls to $0.15. The calculation excludes polishing, welding, inserts, and machine downtime. U.S. Department of Energy die-casting assessments repeatedly identify maintenance and unplanned stoppages as important cost drivers. A mold with a longer theoretical life may still produce poor ROI if repairs interrupt a critical production run.

Maintenance should be planned before the first shot. Inspect parting lines daily, clean vents regularly, and monitor cooling channels for scale. Keep records for flash, porosity, soldering, and dimensional drift. NADCA guidance supports preventive inspection because small defects often become expensive damage. Still, 200,000 shots is not a promise. It depends on alloy, cycle time, die temperature, lubrication, and operator discipline. A cheaper mold may win on paper, yet fail earlier. That uncomfortable possibility deserves a real production trial.

How to Choose the Best Aluminum Die Cast Mold? - Select Mold Life and Cost: 100,000–200,000 Shots, Maintenance, and ROI

Selection Dimension 100,000-Shot Die 150,000-Shot Die 200,000-Shot Die Why It Matters
Typical application Prototype validation, replacement parts, and low-volume programs Stable production with moderate annual demand High-volume production and long-running programs The expected production volume should exceed the planned die life with a reasonable safety margin.
Recommended die construction H13 or equivalent hot-work tool steel; standard inserts and simplified cooling H13 or equivalent steel; replaceable wear inserts and balanced cooling channels Premium hot-work steel; replaceable cores, optimized cooling, and wear-resistant surface treatment Thermal fatigue, soldering, erosion, and dimensional wear are the main die-life limitations in aluminum die casting.
Estimated initial die cost US$25,000–45,000 US$45,000–80,000 US$70,000–130,000 Actual pricing depends on part size, cavity count, slides, ejector complexity, cooling design, steel grade, and machining requirements.
Planned maintenance budget US$10,000–20,000 over die life US$20,000–40,000 over die life US$35,000–70,000 over die life The budget normally covers polishing, vent cleaning, ejector replacement, insert repair, welding, and dimensional correction.
Routine inspection interval Every 10,000–15,000 shots Every 10,000–15,000 shots Every 10,000–15,000 shots, with more detailed records Regular inspection helps identify soldering, cracks, blocked vents, damaged ejector pins, and cooling restrictions before failure.
Major service interval Approximately every 30,000–50,000 shots Approximately every 40,000–60,000 shots Approximately every 50,000–70,000 shots Service timing changes with alloy, casting temperature, lubricant, cycle time, injection speed, and thermal control.
Estimated total tooling cost US$35,000–65,000 US$65,000–120,000 US$105,000–200,000 Total tooling cost combines the initial die price and planned maintenance, excluding machine, labor, alloy, energy, and scrap costs.
Tooling cost per shot US$0.35–0.65 US$0.43–0.80 US$0.53–1.00 Calculated as estimated total tooling cost divided by expected shots; it does not include production operating costs.
Expected dimensional stability Good when process conditions are tightly controlled Very good with scheduled insert and cooling maintenance Very good when thermal management and preventive maintenance are documented Die life alone does not guarantee quality; process control, die temperature, lubrication, and cooling balance are equally important.
Downtime risk near end of life Medium to high if maintenance is deferred Medium with planned spare inserts and service windows Low to medium when critical wear components are replaceable Replaceable inserts and a documented spare-parts plan can reduce unplanned production interruptions.
Best ROI condition Forecast demand is below approximately 80,000–90,000 shots Forecast demand is approximately 90,000–140,000 shots Forecast demand is above approximately 140,000 shots and downtime is costly The best ROI usually comes from matching die life to verified demand rather than selecting the longest possible life.
Recommended decision Choose when capital spending must be minimized and volume is uncertain. Choose for a balanced combination of purchase cost, serviceability, and production life. Choose when annual volume, quality requirements, and downtime losses justify the higher investment. Request a die-life guarantee, maintenance schedule, spare-insert list, inspection criteria, and total-cost quotation before approval.
Planning note: Cost and life figures are typical engineering planning ranges for aluminum cold-chamber die-casting tooling. Actual results vary with part geometry, alloy, die temperature, injection parameters, lubrication, cooling design, production cycle, and maintenance quality.
CAMaster Logo