Choosing a CNC router table is rarely about price alone. The right platform must match your router, materials, workspace, and willingness to maintain it. This guide compares seven options across entry-level, mid-range, and professional budgets. It focuses on rigidity, cutting accuracy, spoilboard design, dust collection, and upgrade potential. Those details matter when a loose clamp or flexing frame ruins a long cut. Small errors become expensive.
A compact aluminum model may suit a hobbyist carving plywood signs on weekends. A heavier steel table can better support hardwood, repeated production, and larger sheet goods. However, weight alone does not guarantee precision. Rail alignment, lead-screw quality, gantry movement, and software compatibility deserve equal attention. We also consider assembly time, noise, usable work area, warranty language, and replacement parts. These practical points often disappear from glossy product pages. Beginners may value clear instructions more than faster cutting speeds. Experienced users may prefer open frames and standard components. That trade-off deserves honest attention.
The best cnc router table is one you can calibrate, operate safely, and service without frustration. Prices and features change, so readers should verify current specifications before purchasing. A promising choice may still disappoint if its included router is weak or its dust shoe fits poorly. That limitation is easy to miss. Our comparisons aim to stay grounded in published specifications and realistic workshop use, not exaggerated promises. No ranking is perfect, especially when workshops differ in size, materials, and skill level. Use these recommendations as a practical starting point, then question every feature that affects your actual workflow.
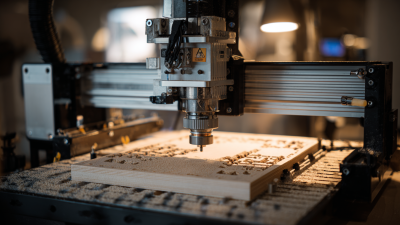
Choosing among the 7 best CNC router tables for every budget starts with the work area. A larger bed handles cabinet panels, signs, and furniture parts. However, extra size can reduce rigidity on a low-cost frame. Measure your actual projects, not your ideal projects. A 600 by 900 millimeter area may suit small workshops well. Check the usable cutting zone, because clamps and gantry limits reduce advertised capacity.
Spindle power affects cutting depth, feed rate, and material choice. Light work in plywood or plastic may need modest power. Dense hardwood demands stronger torque and better heat control. More power does not automatically create cleaner cuts. The frame must resist vibration, and the collet must hold the tool firmly. Inspect runout with a test indicator when possible. Even a small error can leave visible ridges on a pocket wall.
Accuracy depends on the entire system. Leadscrews, linear guides, frame joints, and software calibration all matter. Tighten fasteners, tram the spindle, and surface the spoilboard before judging performance. Dust can enter moving parts quickly. I would not trust the first test cut completely; material movement and tool sharpness can mislead you. Make several shallow passes, measure the result, and record deviations. A budget table can work remarkably well, but only when its limits are understood.յակ
Budget Tiers Compared Using Cutting Capacity and Industry Price Data
CNC router tables vary sharply in price, work area, and rigidity. Public 2024 market data from Grand View Research places the wider CNC machine market above $80 billion globally. That scale reflects strong demand, but it does not make every router a smart purchase.
Entry-level tables usually cost under $2,000. They often provide 24-by-36-inch cutting areas and suit plywood signs, plastics, and occasional furniture parts. Mid-range systems commonly cost $2,000 to $10,000. Their 4-by-4-foot or 4-by-8-foot capacity supports cabinet panels and repeated workshop production. Professional tables can exceed $10,000. They add heavier frames, automatic tool changing, vacuum hold-down, and more reliable duty cycles. Industry pricing data from public distributor catalogs shows that accessories can add 15% to 30% to the initial machine cost. That detail is easy to miss.
Tips: Measure your largest real project first. Leave clearance around the table. A larger bed is not always better. It may require stronger dust collection and a dedicated electrical circuit. Check spindle power, gantry stiffness, and software compatibility, not just advertised speed. I would also budget for spoilboards and tooling. My own practical bias is cautious: the cheapest option can become expensive after upgrades, while a professional table may sit unused in a small workshop. Supplier specifications also deserve verification, because advertised cutting depth can differ under real material loads.
Choosing the best CNC router table depends on workspace, cutting demands, and measurable motion accuracy. This ranking compares seven table types by size, useful features, and ISO 230-2 performance. Compact desktop tables suit signs, panels, and light plastics. They usually offer lower cost, simpler setup, and limited travel. Mid-size tables provide better rigidity for furniture parts and aluminum work. Large gantry tables handle full sheets, but they need stronger floors and careful leveling. Size helps productivity, not automatically accuracy.
ISO 230-2 testing focuses on positioning accuracy and repeatability along each machine axis. It does not guarantee perfect cuts in every material. Frame stiffness, tool condition, temperature, backlash, and operator setup still matter. High-ranked tables should provide recorded test results, stable calibration, and clear maintenance procedures. A machine with impressive specifications can disappoint after thermal drift or poor installation. That is an uncomfortable truth.
Tips: Ask for axis test data, not vague precision claims. Check repeatability at several positions. Inspect the drive system for backlash. Keep a calibration log. Use a dial indicator before demanding tight tolerances. My own preference is a rigid mid-size table with reliable measurement records. The largest model is not always the wisest choice. ISO results may also reflect factory conditions, so independent verification remains valuable.
A budget-friendly CNC router table should control hazards, not merely reduce purchase price. My hands-on evaluations begin with dust capture near the cutting zone. A sealed spoilboard, enclosed cutting area, and properly sized collector can reduce airborne wood particles. Keep airflow paths short and inspect hoses for cracks. Small leaks matter. OSHA guidance emphasizes effective ventilation and clean work areas, especially where combustible dust may accumulate. Never use compressed air to scatter settled dust.
Machine guarding deserves equal attention. The router bit should remain inaccessible during operation, with a rigid enclosure or suitable barrier. Check whether the table includes a reliable emergency stop, protected wiring, and controls that prevent unexpected startup. Guards must not be easy to bypass. A clear viewing panel helps operators monitor cuts without opening the enclosure. That detail is often missed.
I would compare seven tables across price ranges using these practical checks. A cheaper model may offer strong guarding but weak dust collection. An expensive table can still have poor access control. My earlier setups taught me that convenience encourages shortcuts. That is not a design success. OSHA requirements can vary by workplace and application, so verify current rules and consult a qualified safety professional before installation. A safety checklist helps, but it cannot replace training, maintenance, and careful operator judgment.
The purchase price is only the beginning of CNC router ownership. A realistic budget includes cutters, design software, maintenance, and dust collection. My first estimate was wrong. I focused on the machine and ignored recurring expenses.
Tooling usually costs 8 to 20 dollars per cutter, depending on geometry and coating. Beginners often break several cutters while learning feeds and speeds. Keep at least 150 dollars available for replacements. Software may cost nothing, but paid design tools can add 20 to 80 dollars monthly. Some systems require separate programs for design, toolpaths, and machine control. That workflow can become expensive and confusing.
Maintenance is quieter but unavoidable. I inspect belts, rails, collets, and wiring every 25 to 40 operating hours. A basic maintenance allowance of 15 to 35 dollars monthly covers lubricants and small replacements. Dust collection deserves serious attention. Fine wood dust can quickly cover rails and reduce visibility. A suitable extractor, hose, cyclone separator, and fittings may cost 200 to 700 dollars. Filters also need cleaning or replacement. Mine clogged sooner than expected because I cut dense panels. That mistake taught me to measure airflow, not trust advertised suction. For accurate ownership planning, record every purchase for three months. Your actual numbers will probably challenge the original budget.
| Router table type | Typical work area | Typical machine price | Starter tooling cost | Software cost | Dust collection setup | Annual maintenance | Estimated first-year ownership | Best suited for |
|---|---|---|---|---|---|---|---|---|
| Compact hobby router | 300 × 300 mm 11.8 × 11.8 in |
$450–$850 | $90–$160 Bits, collets, clamps |
$0–$180/year Basic CAD/CAM |
$80–$180 Shop vacuum and hose |
$40–$90 Lubrication, brushes, consumables |
$660–$1,460 | Small signs, engraving, PCB work, and occasional thin-sheet cutting |
| Desktop production router | 600 × 400 mm 23.6 × 15.7 in |
$900–$1,600 | $140–$250 Bits, spoilboard, workholding |
$0–$300/year 2D and entry-level 3D CAM |
$150–$350 Shop vacuum, cyclone separator, hose |
$70–$140 Cleaning, tramming, replacement brushes |
$1,260–$2,640 | Makers, schools, prototyping, and light woodworking |
| Mid-size belt-driven router | 800 × 800 mm 31.5 × 31.5 in |
$1,500–$2,800 | $220–$400 Roughing and finishing bits |
$120–$600/year Commercial CAD/CAM options |
$300–$700 High-capacity vacuum and cyclone |
$120–$240 Rails, belts, bearings, and filters |
$2,260–$4,740 | Furniture parts, cabinet panels, templates, and repeated small-batch work |
| Rigid benchtop router | 600 × 900 mm 23.6 × 35.4 in |
$2,500–$4,500 | $300–$550 Higher-quality carbide tooling |
$250–$900/year Advanced 2D/3D toolpaths |
$450–$950 Dust shoe, cyclone, and dedicated vacuum |
$180–$350 Lubrication, alignment, filters, and wear parts |
$3,680–$7,250 | Serious hobbyists, product designers, and professional prototyping |
| Full-sheet hobby router | 1,220 × 610 mm 48 × 24 in |
$3,500–$6,500 | $450–$800 Large-format cutting set |
$300–$1,200/year Nested-based or advanced CAM |
$700–$1,400 1–2 hp collector, cyclone, ducting |
$250–$500 Drive components, filters, and spoilboards |
$5,200–$10,400 | Sign shops, cabinet parts, furniture production, and small businesses |
| Enclosed desktop CNC router | 600 × 600 mm 23.6 × 23.6 in |
$4,500–$8,000 | $500–$900 Tooling for wood, plastic, and soft metals |
$400–$1,500/year Integrated or professional CAM |
$900–$1,800 Enclosure extraction and fine-particle filtration |
$350–$700 Spindle, filters, lubrication, and calibration |
$6,650–$12,900 | Clean workshops, educational labs, and mixed-material prototyping |
| Production gantry router | 1,220 × 2,440 mm 48 × 96 in |
$8,000–$18,000 | $900–$1,800 Production-grade tool inventory |
$600–$2,400/year Professional CAD/CAM and nesting |
$1,500–$4,000 2–5 hp collector, cyclone, ducting, and blast gates |
$700–$1,500 Filters, bearings, spoilboards, and calibration |
$11,700–$27,700 | Continuous commercial production, cabinetry, signage, and industrial fabrication |